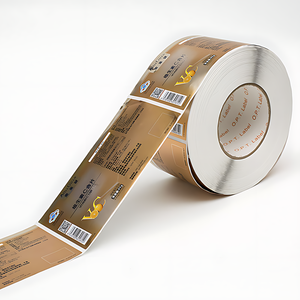
Complete private labeling, short-run digital print options, eco-friendly postal packaging, Amazon FBA prep, and 3PL direct dropshipping.
Strategic Sourcing Analysis: The Evolution of Bulk Capsule Manufacturing in China
The global dietary supplement and pharmaceutical contract manufacturing landscape is undergoing a profound paradigm shift. As consumer demand for wellness products escalates globally, brand owners, pharmaceutical distributors, and e-commerce entrepreneurs are seeking reliable, scalable, and compliant contract manufacturing partners. Navigating the competitive terrain of bulk capsule production requires a sophisticated understanding of manufacturing capabilities, compliance frameworks, quality assurance protocols, and supply chain logistics.
China has established itself as the world’s preeminent hub for bulk capsule manufacturing, leveraging advanced industrial automation, comprehensive raw material supply networks, and rigorous international quality standards. Modern Chinese encapsulation facilities no longer rely solely on cost efficiencies; instead, they lead through technological innovation, offering state-of-the-art Hypromellose (HPMC) vegetable capsules, gelatin shell technology, modified-release enteric delivery systems, and precision micro-encapsulation.
Understanding user intent and market shifts is paramount for procurement directors and brand strategists. Today's international buyers demand transparency, speed-to-market, and strict adherence to regional dietary regulations. The primary drivers transforming contract manufacturing include:
Clean-Label & Vegetarian Dominance: Accelerated shift from traditional bovine/porcine gelatin capsules toward plant-derived HPMC, Pullulan, and Tapioca starch capsule shells to cater to Vegan, Kosher, and Halal consumer segments.
Elimination of Titanium Dioxide (TiO2): In response to European Food Safety Authority (EFSA) bans, top-tier Chinese capsule suppliers have re-engineered opacification technology, employing calcium carbonate and rice starch for compliant shell opacity.
Enhanced Bioavailability Technologies: Rising demand for liposomal encapsulation, liquid-filled hard capsules (LFHC), and dual-capsule-in-capsule technology designed to preserve sensitive botanical extracts, probiotics, and hydro-sensitive active pharmaceutical ingredients (APIs).
Supply Chain Resilience & Low MOQ Flexibility: Brands require agile inventory management. Leading suppliers now offer tiered ordering structures—enabling start-ups to launch with minimum order quantities (MOQ) as low as 10 to 1,000 units, while supporting enterprise runs exceeding tens of millions of capsules.
Technical Quality Assessment Framework for B2B Buyers
To ensure brand integrity and eliminate regulatory friction when importing bulk capsules, global sourcing directors must implement an exhaustive technical audit framework. Adherence to international pharmacopeia standards—including USP (United States Pharmacopeia), EP (European Pharmacopoeia), and ChP (Pharmacopoeia of the People's Republic of China)—is mandatory.
1. Moisture Content & Shell Mechanical Properties
Moisture control is critical to preventing capsule brittleness or cross-linking. Standard hard gelatin capsules require a equilibrium moisture content between 13.0% and 16.0%. Conversely, modern HPMC vegetable capsules maintain a lower moisture spectrum of 4.0% to 7.0%, making them uniquely suited for hygroscopic powders, herbal extracts, and moisture-sensitive probiotic strains.
2. Disintegration Profiling & Dissolution Rate
Quality assurance protocols require strict compliance with USP <701> Disintegration testing. Standard immediate-release capsules must achieve full disaggregation within 15 minutes in simulated gastric fluid (pH 1.2). For targeted intestinal release, specialized enteric-coated capsules undergo two hours of exposure in acidic media without degradation, followed by complete dissolution in simulated intestinal fluid (pH 6.8) within 45 minutes.
High-capacity filling machines operating at speeds up to 150,000 capsules per hour require uniform shell dimensions. Premium factories utilize continuous ultrasonic wall thickness gauging, maintaining length tolerances within ±0.3mm and weight variations under 2.0%, ensuring zero machine jamming and minimal fill-weight variation during high-speed encapsulation.
BRCGS Global Standard CertifiedcGMP Compliant Production100% Quality & Potency Guarantee
Integrated Enterprise Capabilities: From Concept to Global Shelf
Modern B2B purchasing extends beyond bare bulk capsule supply. Leading Chinese factories provide end-to-end contract manufacturing (OEM/ODM) solutions designed to streamline international brand expansion. By integrating raw material sourcing, customized formulation R&D, primary and secondary packaging, and direct market logistics under one operational umbrella, brand owners reduce overhead, shorten product development lifecycles, and mitigate vendor communication errors.
Custom Formulations & Dosage Form Diversification
Whether formulating a high-potency sports nutrition supplement, an anti-aging beauty complex, or a targeted veterinary probiotic, robust R&D teams leverage advanced blending techniques (high-shear wet granulation, dry compaction, micro-pelletization). Available dose delivery formats include:
Hard Gelatin & HPMC Capsules: Sizes 000, 00, 0, 1, 2, 3, 4 with customizable shell colors, banding, and axial/radial logo printing.
Softgels: High-clarity gelatin or vegan carrageenan softgel capsules for lipid-soluble nutrients, omega-3 fish oils, COQ10, and botanical suspensions.
Functional Gummies & Chewables: Pectin-based, non-melting gummy delivery systems for beauty, immunity, and lifestyle health markets.
Packaging plays a decisive role in brand positioning, consumer safety, and shipping efficiency. Advanced OEM suppliers offer diverse primary packaging options, including flat postal bottles engineered for reduced direct-to-consumer parcel freight costs, recyclable PET and HDPE amber bottles, moisture-barrier blister packs (Alu-Alu, PVC/PVDC), and child-resistant closure systems.
Technical Procurement FAQ: Answers for Global Sourcing Managers
What is the baseline Minimum Order Quantity (MOQ) for custom bulk capsule orders?
Our stock formulas and standard capsule sizes start at flexible low MOQs from just 10 to 100 bottles (or equivalent bulk count). For bespoke custom formulations requiring specialized active ingredients or custom-colored printed capsule shells, standard production runs typically start at 100,000 bulk capsules.
How do Chinese manufacturers guarantee compliance with US FDA and EU food safety standards?
Reputable factories operate Class 100,000 cleanrooms certified under BRCGS, ISO 22000, and cGMP guidelines. Every production lot undergoes rigorous analytical testing via High-Performance Liquid Chromatography (HPLC), Atomic Absorption Spectroscopy (AAS) for heavy metals, and automated microbiological screening. Certificate of Analysis (COA) documentation accompanies every batch.
Can you facilitate Amazon FBA prep and international dropshipping services?
Yes. We provide complete turnkey 3PL fulfillment solutions, including FNSKU barcode labeling, master carton compliance packaging, temperature-controlled freight forwarding, and direct-to-consumer dropshipping to major consumer markets worldwide.
What are the shelf-life and storage recommendations for bulk HPMC vs. Gelatin capsules?
When stored in sealed, light-resistant containers at controlled room temperatures (15°C to 25°C) and relative humidity between 35% and 65%, bulk capsules maintain a stability shelf-life of 36 to 48 months. HPMC capsules offer superior stability in humid tropical environments due to their resistance to cross-linking.
What is the standard lead time from initial formulation approval to shipment dispatch?
In-stock formulas with approved customer artwork typically process and ship within 5 to 7 business days. Custom product development projects—including benchtop lab trials, stability testing, raw material sourcing, and label printing—generally require 3 to 5 weeks from final sign-off.
As the global health and wellness sector expands, strategic alignment with a technologically advanced capsule manufacturer is the single most critical factor in ensuring market agility, regulatory protection, and healthy profit margins. Buyers who prioritize verified quality management systems, transparent documentation, and flexible supply agreements will successfully capture emerging consumer trends across global e-commerce and retail channels.
Partnering with China’s top-tier manufacturing eco-system grants global brands direct access to groundbreaking formulation technologies, unmatched production scalability, and comprehensive private labeling expertise—transforming complex supply chains into a sustainable engine for brand growth.
Accelerate Your Brand Launch Today
Consult with our technical contract manufacturing specialists. Receive instant pricing, custom formulation quotes, and free sample kits tailored to your market specifications.